Faced with outdated systems, tight space, and rising energy demands, a leading medical and pharmaceutical distributor partnered with Trew to modernize a 250,000 sq ft fulfillment center. The solution delivered a custom layout, UL-certified equipment, and over 3.5 miles of conveyor powered by CHAMP™ WCS. The result? Streamlined flow, energy savings, and a scalable system that’s already inspiring four new greenfield sites.
The Challenge
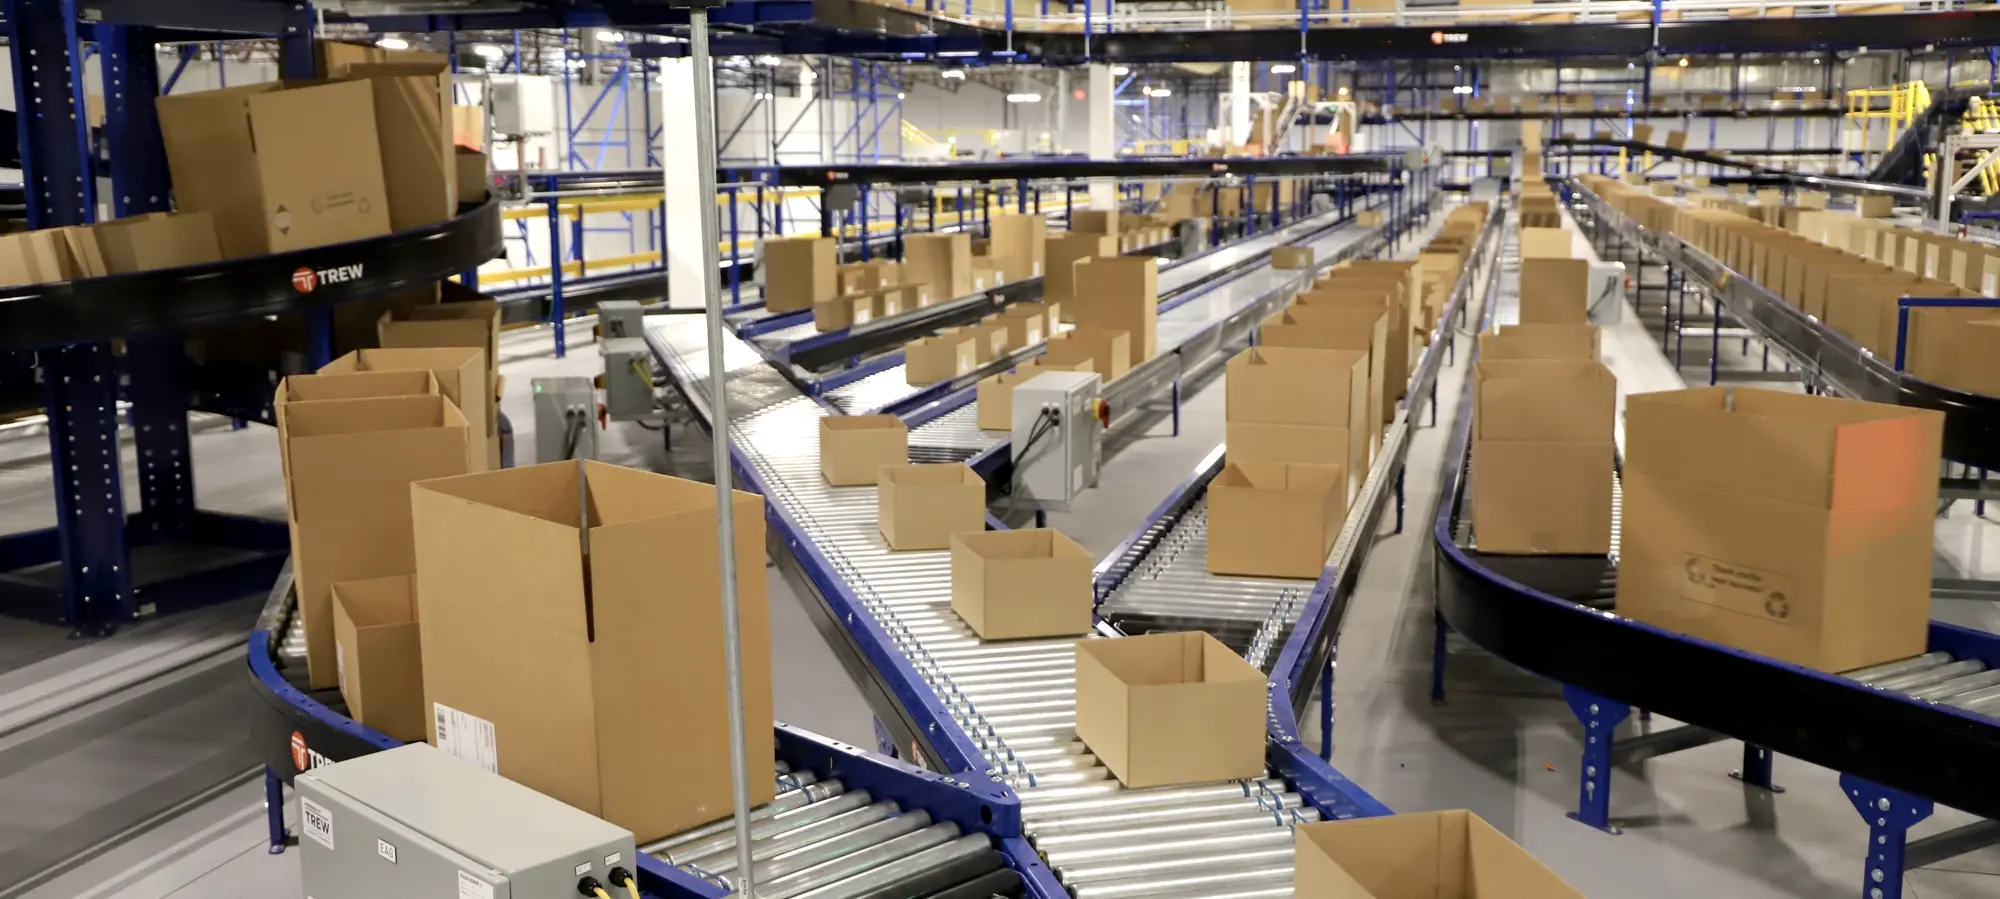
The client’s legacy system was modernized to boost picking efficiency and improve operational flow while designing a custom layout to overcome space constraints. The solution incorporated UL-certified equipment to meet regulatory requirements and delivered energy-saving features that maintained high performance with reduced energy consumption.
The Solution
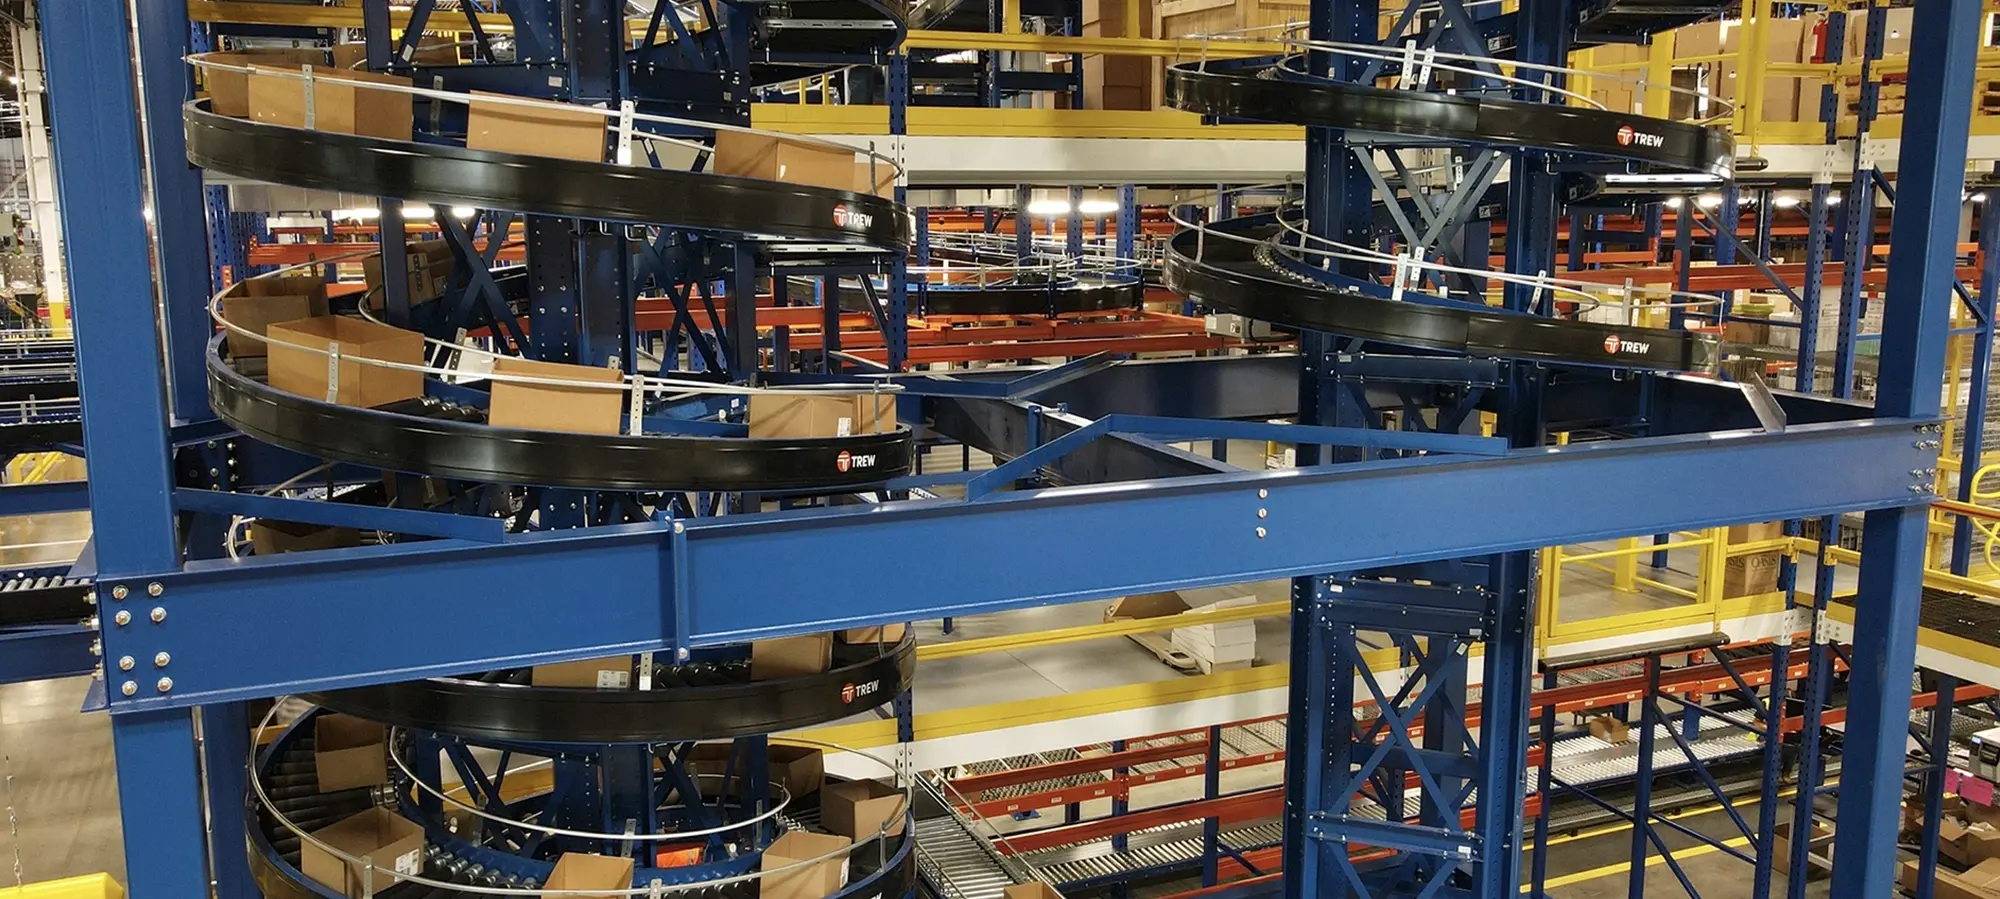
Trew upgraded the system to boost picking efficiency and streamline operations. A customized layout featuring MDR spirals optimized product flow in tight spaces. All equipment was UL-certified to meet compliance standards and energy-saving photo-eyes powered down the system down after inactivity.
The Result
The solution kept rates, volumes, and accumulation in balance to prevent backups, while MDR technology delivered cost and energy savings by running only when products were present. This project’s performance has already sparked plans for added capacity and four new greenfield sites.
Leave a Reply